Shipping Country Estonia - English
CYLINDER RESTORATION
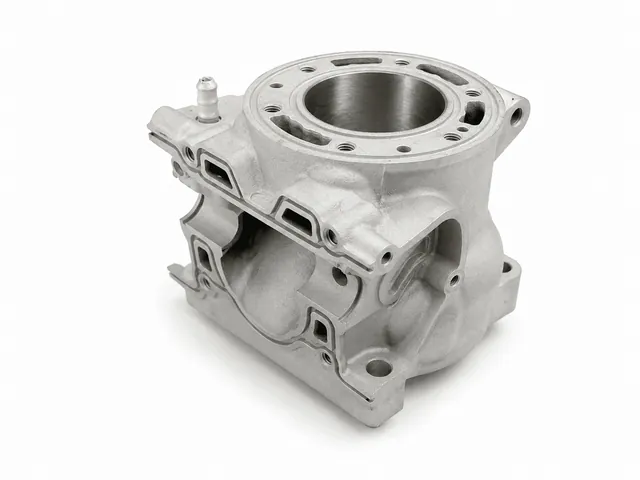
For seized or heavily worn cylinders, we offer all services to restore the internal coating, bringing them back to full functionality.
For light seizures that did not affect the coating, honing is sufficient. Where the coating is damaged or detached, re-chroming is necessary.
At the end of the process, perfect cylindricity is verified and the bore is measured with the cylinder thermostated at 20 °C. Upon request, a dedicated piston can be paired.
Re-chroming
Nickel–silicon coating to restore the inner surface and durability.
Re-chroming restores the internal surface coating (Nickel–Silicon) when the original coating is heavily worn, damaged, or detached in places.
Being an artisanal process, the quality and adhesion to the aluminium’s porosity make it more durable than typical mass-production coatings.
The process includes:
• removal of the previous coating using mild acids and bases (inert to the aluminium)
• stress-relief heat treatment to avoid residual tensions
• turning the bore to restore perfect cylindricity and perpendicularity to the head planes
• deburring of the transfer passages
• electroplating bath to apply the new coating
• sandblasting to remove residues and ensure a perfect surface finish
• heat treatment to verify perfect adhesion
• honing to size and t-shape finish
The price refers only to the operations listed and excludes additional work such as exhaust bridge radiusing, welding, etc.
- 2-stroke cylinders:32–52 mm158,60 €·17 days
- 53–65 mm207,40 €·17 days
- 66–72 mm248,27 €·17 days
- 73–90 mm290,97 €·17 days
- 4-stroke cylinders:66–88 mm248,27 €·17 days
- 89–106 mm290,97 €·17 days
Polishing, Honing & T-shape
Surface restoration with perfect cylindricity and very low roughness.
Honing restores the Nickel–Silicon coating to perfect cylindricity with a very low surface roughness.
The cross-hatched micro-grooves (t-shape) retain oil and ensure optimal lubrication in operation.
This is required whenever a piston is replaced to match the new piston with the correct clearance and a properly restored inner surface.
- Processing cost54,90 €·5 days
Exhaust bridge radiusing
A mandatory step after re-chroming on 2T cylinders with an exhaust bridge.
Radiusing of the exhaust bridge is required after the re-chroming process on 2-stroke cylinders featuring a bridge exhaust.
The bridge, exposed to hot exhaust gases and being thin/elongated, runs hotter and expands more than the cylinder.
Anchored at top and bottom, it can only expand towards the cylinder axis.
In operation, this would quickly damage the piston and reduce its lifespan.
We pre-relieve the bridge by a few hundredths depending on model and displacement.
At operating temperature, the bridge aligns with the bore, ensuring proper function and piston durability.
- Processing cost33,55 €·1 day
Welding
Structural repair for severe seizures (re-chroming excluded).
For severe seizures that also damage the aluminium base, once the coating is removed, aluminium is added by welding to restore the original shape.
Given the delicacy and assessment difficulty (especially for severe damage), it’s best to inspect the cylinder after de-coating to gauge the real extent.
The process includes stress-relief heat cycles to avoid distortion or post-weld cracking.
Welding costs exclude re-chroming, which is necessary because welding is performed on a de-coated cylinder.
- Processing cost63,44 €·10 days
Exhaust bridge reconstruction
Partial/total reconstruction with new material and final heat cycles.
In case of heavy seizures on cylinders with an exhaust bridge, cracking may initiate inside the bridge.
If detected (usually after de-coating), we offer complete reconstruction to restore the top-end’s proper function.
The service includes: partial/total removal of the bridge, addition of new material by welding, hand re-profiling to restore the exhaust duct geometry, and final heat cycles for stress relief.
Reconstruction excludes re-chroming and radiusing, which are necessary because the work is done on a de-coated cylinder.
WARNING: Honda CR125 (2000–2004) and CR250 (2002–2004) cylinders suffer a design issue that tends to create cracks in the exhaust bridge.
Our reconstruction solves the issue in ~80% of cases; however, because it is a structural design flaw, we cannot guarantee long-term durability for the remaining ~20%.
Therefore, this is the best available option, but no durability guarantee can be provided since the defect is due to the manufacturer’s design.
- Processing cost170,80 €·13 days
Bore enlargement
Boring the liner to a specified size for performance gains.
For those who seek more power, we offer cylinder enlargement.
Once feasibility is confirmed, the de-coated cylinder bore is machined to the target size.
Feasibility depends on removable stock and residual structural rigidity.
It is the customer’s responsibility to ensure the upgrade’s feasibility and compatibility of other components.
The enlargement cost excludes re-chroming, which is necessary since the bore is machined on a de-coated cylinder.
- Processing cost30,50 €·1 day
MATING SURFACE MACHINING
CNC resurfacing of PAT/PAC cylinder planes to restore or modify.
Machining of the cylinder’s planes—PAT (head plane) and PAC (crankcase plane)—to restore damaged surfaces or modify heights.
Performed on CNC lathes to ensure perfect flatness of the mating surfaces.
The process also restores any head cover planes and O-ring grooves.
- Processing cost50,02 €·5 days
ANTI-DETONATION RING
Adding a bronze ring on the top plane to reduce detonation.
For highly tuned engines or detonation issues, a bronze ring can be installed on the top plane to significantly raise the detonation threshold. The mod, from racing, creates a groove where a bronze ring is interference-fitted and then ground to align perfectly with the bore.
Thanks to the metal’s properties, auto-ignition is reduced and erosion of the head plane is avoided.
If a cylinder already has the ring, re-installation is required after re-chroming.
- Processing cost115,90 €·5 days